Disclosure: As an Amazon Associate, Reviews Took earns from qualifying purchases. Links to Amazon on this page are affiliate links; they cost you nothing extra.
Check input voltage and wire types.
This guide is built from Amazon product listings and maker specs, not our own testing, so confirm size, contents and current price on each product page.
Check the current price on Amazon for each pick.
Last updated: November 2, 2026.
In this guide
Quick Picks
| Product | Type | Best for |
|---|---|---|
| YESWELDER 205A MIG Welder | MIG welder | home welding |
| BESTMIG 145A 4-in-1 Multi-Process Welder | MIG welder | home welding |
| ANDELI 110V/220V PULSE Flux Core MIG Welder 135A,Gasless MIG Stick | MIG welder | home welding |
| 145A MIG Welder 110V 3-in-1 Flux Core Stick Lift TIG 7.5 lb | MIG welder | home welding |
| YESWELDER 160A MIG Welder | MIG welder | home welding |
| BESTMIG 135A MIG Welder – 3-in-1 Flux Core Welder | MIG welder | home welding |
| YESWELDER 135A MIG Welder | MIG welder | home welding |
| 160Amp 3 IN 1 Welder | MIG welder | home welding |
Our Picks

Top pickBest for home welding
1. YESWELDER 205A MIG Welder
A YESWELDER 205A MIG Welder (mig welder), per the listing. Check price on Amazon.
Good for: home welding. Watch out: Check duty cycle.


Best for home welding
2. BESTMIG 145A 4-in-1 Multi-Process Welder
A BESTMIG 145A 4-in-1 Multi-Process Welder (mig welder), per the listing. Check price on Amazon.
Good for: home welding. Watch out: Check duty cycle.

Best for home welding
3. ANDELI 110V/220V PULSE Flux Core MIG Welder 135A,Gasless MIG Stick
An ANDELI 110V/220V PULSE Flux Core MIG Welder 135A,Gasless MIG Stick (mig welder), per the listing. Check price on Amazon.
Good for: home welding. Watch out: Check duty cycle.

Best for home welding
4. 145A MIG Welder 110V 3-in-1 Flux Core Stick Lift TIG 7.5 lb
A 145A MIG Welder 110V 3-in-1 Flux Core Stick Lift TIG 7.5 lb (mig welder), per the listing. Check price on Amazon.
Good for: home welding. Watch out: Check duty cycle.


Best for home welding
5. YESWELDER 160A MIG Welder
A YESWELDER 160A MIG Welder (mig welder), per the listing. Check price on Amazon.
Good for: home welding. Watch out: Check duty cycle.


Best for home welding
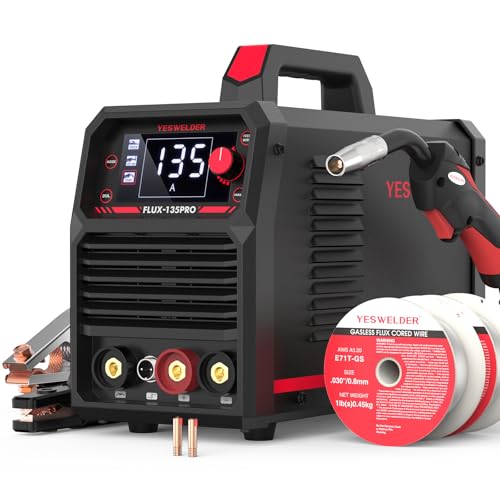
6. BESTMIG 135A MIG Welder – 3-in-1 Flux Core Welder
A BESTMIG 135A MIG Welder – 3-in-1 Flux Core Welder (mig welder), per the listing. Check price on Amazon.
Good for: home welding. Watch out: Check duty cycle.

Best for home welding
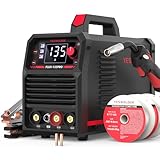
7. YESWELDER 135A MIG Welder
A YESWELDER 135A MIG Welder (mig welder), per the listing. Check price on Amazon.
Good for: home welding. Watch out: Check duty cycle.
Best for home welding
8. 160Amp 3 IN 1 Welder
A 160Amp 3 IN 1 Welder (mig welder), per the listing. Check price on Amazon.
Good for: home welding. Watch out: Check duty cycle.
Best Picks by Category
These labels summarize listing details and are not hands-on test results.
- Highest listed rating (limited feedback): BESTMIG 145A 4-in-1 Multi-Process Welder. This is not an independent product-quality award.
- Most reviewed: YESWELDER 135A MIG Welder.
- Best value: 145A MIG Welder 110V 3-in-1 Flux Core Stick Lift TIG 7.5 lb — a budget-tier pick.
- Lowest price: 145A MIG Welder 110V 3-in-1 Flux Core Stick Lift TIG 7.5 lb — a budget-tier pick.
- Premium option: YESWELDER 205A MIG Welder — a premium-tier pick.
Price, Rating and Review Comparison
The table lists the picks with their price tier. Prices change often, so check price on Amazon to confirm the current price.
| Product | Price | Rating | Ratings | Price tier |
|---|---|---|---|---|
| 145A MIG Welder 110V 3-in-1 Flux Core Stick Lift TIG 7.5 lb | Check price on Amazon | — | — | Budget |
| 160Amp 3 IN 1 Welder | Check price on Amazon | — | — | Mid-range |
| ANDELI 110V/220V PULSE Flux Core MIG Welder 135A,Gasless MIG Stick | Check price on Amazon | — | — | Mid-range |
| BESTMIG 135A MIG Welder – 3-in-1 Flux Core Welder | Check price on Amazon | — | — | Mid-range |
| YESWELDER 135A MIG Welder | Check price on Amazon | — | — | Mid-range |
| BESTMIG 145A 4-in-1 Multi-Process Welder | Check price on Amazon | — | — | Mid-range |
| YESWELDER 160A MIG Welder | Check price on Amazon | — | — | Premium |
| YESWELDER 205A MIG Welder | Check price on Amazon | — | — | Premium |
How Much Feedback Backs Each Rating
Check the listing on Amazon for current feedback on each pick.
How to Choose
Rating
Check amps, size or power ratings.
Build
Heavier materials last longer.
Safety
Use protective gear and follow instructions.
Shielding Gas Versus Flux-Core Wire
The first decision for a new MIG welder is how the weld pool will be protected from the air. Solid wire used with a shielding gas produces clean welds with little spatter and almost no slag, and it works well on thin to medium steel in a workshop. It needs a gas cylinder, a regulator and a hose, and the gas can be blown away by wind, so it suits indoor work. Flux-core wire has flux inside the wire that makes its own shielding as it burns, so no gas bottle is needed. It copes with outdoor conditions and slightly dirty metal better, but it makes more smoke and spatter and leaves slag to chip off.
Many beginner machines are sold as combination units that can run either way. The difference is polarity: gas welding and flux-core welding use opposite polarity connections, and the machine usually has a lead you move to switch. Read the manual to learn how to do this, and check the listing to see whether both processes are supported. Some machines are described as gasless only, so they cannot be used with a bottle.
Think about where you will weld. A garage with a closed door and a bottle of gas suits clean work on car panels, brackets and furniture. A yard or a driveway where wind is a concern, or a repair job on rusty farm equipment, may suit flux-core. If you start with flux-core to save the cost of gas, expect more cleanup, and consider adding a gas setup later if the machine allows it.
Power Input, Material Thickness and Duty Cycle
The power supply you have limits the machine you can use. Some welders run on standard household 120-volt outlets, which suits small projects, while others need a 240-volt supply, which can weld thicker material. Dual-voltage machines accept either, with an adapter or a switch. Check the listing for the input requirements, and check your outlet and circuit breaker. Running a high-demand machine on a weak circuit trips the breaker and can cause overheating of wiring.
Listings usually state the thickness of steel the machine can weld. Treat that as the maker’s rating under good conditions. Thicker material needs more power and often multiple passes, and a small machine struggles with it. Think about your first projects, such as sheet metal repairs, small frames or tabletops. Choose a machine whose range comfortably covers them, with some margin.
Duty cycle describes how long the machine can weld in a ten-minute period before it needs to cool down, and it is given at a specific current. A lower duty cycle at high current means the machine will stop for cooling more often, which is common on small welders. For short beginner jobs this is rarely a problem, but long runs on thick material will hit the limit. Check the duty cycle, and read what the maker states about thermal protection. Allow the machine to cool when it signals, and do not block the vents.
Controls, Settings and Ease of Setting Up
Getting the settings right is what frustrates beginners most. Voltage controls the arc length and heat, and wire speed controls how much wire feeds into the pool. They must be balanced. Many machines have a chart inside the wire door that suggests settings for different thicknesses, and you adjust from there by listening to the arc. A smooth, steady crackle, like frying bacon, is the sound that welders often describe as right.
Some machines have synergic or one-knob controls, where the machine suggests wire speed based on the voltage or material thickness you select. These can simplify learning, but you should still check how adjustable they are, and whether you can fine tune. Digital displays can make settings repeatable, while stepped dials with taps are simple and robust. Neither is better in all cases.
Look at the practical details. A clear manual, a settings chart, and an easy wire loading path make setup less daunting. Check the type of drive roll, how the tension is adjusted, and whether the gun is easy to hold. A longer cable gives reach, but a very long cable can add resistance. Look at whether the ground clamp is sturdy, because poor grounding causes erratic arcs. Spend time on test pieces of scrap before welding a real project.
Wire, Tips, Liners and Other Consumables
MIG welding consumes parts, so check what the machine uses before buying. Wire comes on spools of certain diameters and weights, and the machine only accepts the sizes it is built for. Thinner wire suits thin metal, and thicker wire suits heavier work. Make sure you buy the correct wire type for your process, since solid wire and flux-core wire are not interchangeable in a machine set up for one or the other.
Contact tips wear out and should be replaced regularly. They guide the wire and pass current to it, so a worn tip causes erratic feeding and a rough arc. Nozzles collect spatter and need cleaning. Liners guide the wire through the gun cable, and a clogged or kinked liner causes feeding trouble. Check that these parts are standard and easy to find, and consider buying spares with the machine.
Drive rolls grip the wire, and the groove must match the wire type and size. Using the wrong groove can crush or slip the wire. Keep wire dry, because rust on the wire causes poor welds. Cover spools when not in use. Gas users also need to think about regulators, hoses and cylinder refills or exchanges. Check the local availability of cylinders, and learn how to store and move them safely, upright and secured.
Safety, Practice and Fixing Common Problems
Welding carries real risks, so equip yourself properly. You need a welding helmet with the right shade, welding gloves, a flame-resistant jacket or long sleeves, and sturdy shoes. Weld in a ventilated space, and keep flammable materials well away. Keep a fire extinguisher nearby. Fumes can be harmful, particularly from coated or galvanized metals, so clean the metal and do not weld material when you do not know what it is. Read the machine’s manual before the first arc, and ask an experienced welder or a training course for guidance.
Practice on scrap of the same thickness as your project. Aim for a consistent travel speed, steady gun angle and stick-out. Clean the metal of rust, paint and oil, and make sure the ground clamp is attached to bare metal. Practice beads in a straight line, then simple joints such as lap and T joints. Cut or grind welds to examine penetration, and adjust settings accordingly.
Common beginner problems have common fixes. Wire that stutters or burns back to the tip may signal a worn tip, wrong tension or settings. A lot of spatter may mean voltage and wire speed are off, or that the metal is dirty. Porosity, which shows as small holes, suggests poor gas coverage or contamination. Weak, ropey beads often mean too little heat. Replace the machine or send it for service when cables are damaged, the unit smells hot or trips often, or the wire will not feed even with new consumables. Check the warranty terms in the listing.
Reading a Welder Listing Line by Line
A welder listing packs a lot into a few bullet points, and the order they appear in is not always the order that matters. Begin with the input voltage, because a machine that only runs on a dedicated high-power circuit may not suit a garage with ordinary outlets. Next look at the amperage range and the thickest steel the maker says it can join in a single pass. Those two numbers tell you whether a machine fits your projects far better than a flashy title does.
Then scan for the process list. Many machines in this class advertise several modes, such as gas-shielded MIG, gasless flux-core and stick. A multi-mode machine gives you room to grow, but every extra mode adds menus and accessories to learn. Finally, check what is actually in the box. Some kits include a gun, ground clamp, hood and a small spool of wire, while others leave you to buy those pieces separately.
Which Project Calls for Which Setup
| Project | Sensible approach |
|---|---|
| Thin sheet metal repairs | Low amperage range with fine control |
| Garden gates and railings | Mid-range machine with flux-core for outdoor breeze |
| Trailer and frame work | Higher amperage and a dedicated circuit |
| Small shop fixtures and tables | Gas-shielded MIG for cleaner beads |
| Occasional fix-it jobs | Compact multi-process unit that stores easily |
If your projects vary a lot, lean toward a machine with a wider adjustment range. If you will mostly repeat one kind of job, a simpler machine with clear presets will get you to a decent weld sooner.
A Practice Plan for the First Few Sessions
- Gather scrap steel of the same thickness you plan to weld and clean it down to bare metal.
- Read the settings chart inside the machine or manual and begin there rather than guessing.
- Run straight beads on flat plate until the sound is a steady crackle rather than loud pops.
- Try a simple lap joint, then cut it apart to see how deep the weld went.
- Only then move on to real parts, and clamp them firmly before each weld.
Always wear a proper welding helmet, gloves and flame-resistant clothing, work in a ventilated space away from anything flammable, and follow the maker’s instructions and local codes for electrical connections. If the circuit in your workshop is uncertain, ask a licensed electrician before plugging in a high-draw machine.
Cleaning Up After a Session
Good habits after welding extend the life of the machine and make the next session smoother. Let the gun and cable cool before you coil them loosely, because tight bends can kink the liner. Wipe spatter from the nozzle with the tool the maker supplies, and check the contact tip for wear. Pull the wire back onto the spool or cover it to keep dust and moisture away. Store the unit in a dry place off the concrete floor, and keep the manual close so you can look up consumable part numbers when they run low.
Setting Up Your First Welding Bench and Workflow
A beginner’s results depend as much on the workspace as on the machine, so set the bench up properly before the first arc. You need a steel-topped surface or a proper welding table, clear of anything flammable, with room for the work, the clamps and the ground clamp lead to reach comfortably. Position the welder so its controls face you and its fan vents are unobstructed, and route the cables so they cannot be stood on or tripped over mid-weld. Good layout feels unremarkable, which is the point: nothing should compete for your attention while you are learning to watch the puddle.
Organise the consumables within arm’s reach: spare contact tips, a tip cleaner or reamer, pliers for trimming wire, a wire brush and a chipping hammer if you run flux-cored wire. Beginners lose their rhythm, and their temper, hunting for a tip while the work cools. A small tray or magnetic dish on the bench keeps these items together. Keep the helmet, gloves and jacket in one place too, so the safety routine of putting them on becomes automatic rather than negotiated each session.
Plan the work itself in a fixed order: cut, clean, fit, clamp, tack, weld, cool, inspect. Following the same sequence every time builds habits that protect quality, because most bad beginner welds are decided before the arc starts, by dirty metal, poor fit-up or missing clamps. The project-matching guidance earlier in this guide tells you which process and settings suit each job; this workflow is how you give that choice a fair chance to succeed on the bench.
Reading Your Beads: A Beginner’s Diagnostic Guide
Learning to weld is mostly learning to read beads, so develop the habit of inspecting every practice weld before grinding anything away. A good bead is uniform in width, ties into both pieces at the edges, and has a consistent ripple. When a bead sits tall and ropey on the surface, the usual causes are travel speed too fast, voltage too low for the wire speed, or an arc length held too long. Slow down, check the settings chart inside the machine’s door, and change one variable before the next pass.
Holes and porosity tell a different story. With gas-shielded welding, porosity usually means the shielding was lost: a draught, a clogged nozzle, gas flow wrong or the gas simply off. With flux-cored wire, suspect damp wire, contaminated metal or too long a stick-out. Undercut, a groove melted into the edge of the joint, points to excessive heat or a travel angle that washes metal away from the edge. Each defect has a short list of likely causes, and working through them calmly, one at a time, is exactly how experienced welders troubleshoot too.
Keep a practice notebook, at least at first. Note the material thickness, the wire, the settings and what the bead looked like, and keep one sample piece from each session. Within a few weeks you will own a personal settings reference more useful than any generic chart, because it describes your machine, your mains supply and your hand. The multi-process machines in this guide all reward this methodical approach; their extra processes simply give the notebook more chapters over time.
The Projects That Teach the Most in Your First Months
Choose early projects for the lessons they teach, not just their usefulness. A simple welding cart or a small steel stool teaches cutting lists, squareness, tacking and welding in several positions, and it remains useful in the shop forever. Repairing a gate hinge or a garden tool teaches preparation on imperfect, real-world metal, which is a different and equally valuable skill. Alternating a clean fabrication project with a grubby repair project rounds a beginner out faster than either alone.
Scrap practice should be structured, not random. Run beads on flat plate until they are consistent, then butt joints, then fillet joints on angle iron, then vertical and overhead positions only when the flat work is genuinely sound. Each stage exposes a new variable while the previous skills hold steady. Rushing to a trailer hitch or a structural repair before those stages are complete is the classic beginner error, and the safety guidance in this guide exists largely to prevent it: learn on work where failure costs nothing.
Know which jobs to decline in the first year. Anything whose failure could hurt someone, vehicle frames, lifting points, pressure vessels, structural building work, belongs to qualified welders until your skills are proven and, where required, certified. A beginner machine from this guide is entirely capable of excellent work within its proper scope: furniture, brackets, garden structures, art, and light repairs. Staying inside that scope is not a lack of ambition; it is how welders build the record that eventually earns the bigger jobs.
Wire, Gas and Consumables: Buying and Storing Them Well
Consumables are a running cost that beginners underestimate, so buy them with the same care as the machine. Wire should be bought in sizes matched to your work, stored dry and used in rotation, because damp or rusty wire feeds badly and welds worse. Keep spools in their bags or a sealed box with the desiccant they came with, and never leave a spool sitting in a damp garage through winter and expect clean welds from it in spring. The wire guidance earlier in this guide covers types and sizes; storage is what protects that investment.
If you run gas, treat the bottle as part of the workshop’s safety system. Bottles stand upright, secured against falling, with caps on when moved, and regulators are fitted and checked rather than assumed. Renting versus buying a bottle depends on how much you weld, and either is legitimate; what matters is never letting an empty bottle surprise you mid-project, and never using a gas or regulator combination the supplier has not approved for the process.
Contact tips, nozzles and liners wear quietly and then fail loudly. A tip that has become oval makes the wire wander and the arc unstable, and beginners often blame their technique for what is actually a worn consumable costing very little. Replace tips on suspicion, keep the nozzle clean of spatter, and learn how your machine’s liner is changed before the day it must be changed urgently. The machines above all use widely available consumables, which is one of the most practical reasons they suit beginners.
Choosing Among the Machines Above for Your Real Work
The eight machines in this guide separate less by quality than by emphasis, so match them to the work you described in your project list. If nearly everything you plan is home and garden steel work, a straightforward machine with a strong flux-cored performance and simple controls will serve you better than a feature-rich model whose extra processes you never touch. Simplicity at the panel means more of your attention stays on the puddle, which is where learning happens.
If your plans genuinely span processes, repairs one month, a fabrication project the next, some stick work outdoors, then the multi-process models earn their complexity, provided you accept the setup changes each process involves. Read the individual reviews above for how each machine handles those changes, because a process you dread setting up is a process you will not use. Dual-voltage flexibility matters if your workshop power is limited or you expect to weld at other locations.
Finally, think about support and consumables in your area. A machine whose tips, liners and parts are easy to obtain locally or by quick delivery will spend its life welding; an obscure machine waits for parts. The brands in this guide were chosen partly for that accessibility. Buy the machine that fits your projects, your power supply and your patience for setup, in that order, and it will still be the right machine when your skills have doubled.
Ground Clamps, Cables and the Electrical Path Nobody Thinks About
Beginners blame settings for problems that live in the electrical path. The ground clamp must bite clean, bright metal, close to the weld, with its cable undamaged and its connection to the machine firm. A clamp hanging off a rusty edge by one tooth forces the arc to hunt for a path, and the resulting instability looks exactly like poor technique. Before any session, give the work lead the same inspection you give the gun: cable sound, clamp jaws clean and springy, connection tight.
Cable management matters too. Coiled leads, leads run underfoot, and a gun cable kinked sharply at the machine all create faults that appear and vanish confusingly. Lay cables out in gentle curves, keep them out of the welding zone’s traffic, and never wrap the work lead around the machine to store it in a way that strains the connection. These are thirty-second habits that remove a whole category of mysterious bad days.
Welding Positions: Flat First, Then Honestly Upward
All beginner instruction assumes the flat position because gravity helps the puddle there, and your early projects should respect that: design and clamp work so as many joints as possible can be welded flat or horizontal. Rotating the work is almost always easier than fighting gravity with an unpractised hand. A simple positioner is beyond most home shops, but a bench, blocks and clamps can turn most small fabrications to present their best side.
When you do progress to vertical and overhead work, expect to relearn heat control at lower settings with smaller, faster beads, and practise on scrap in position before touching a project. Overhead welding also changes the safety picture completely, since sparks and spatter fall on the welder: full protective clothing, no gaps at collar and cuff, and a cap under the helmet stop being optional. Earn these positions gradually and they become skills; rush them and they become the reason beginners quit.
Measuring, Marking and Cutting: The Skills Before the Skill
Welding quality is capped by preparation quality, and preparation is mostly measuring, marking and cutting. Learn to mark steel clearly with a soapstone or fine marker that survives handling, to cut with a guide rather than by eye alone, and to check for square before tacking, because a frame tacked out of square will be welded out of square with great consistency. The time to discover a miscut piece is at the dry fit, not with the arc running.
Deburr and bevel where the joint needs it. Thin material needs clean, tight edges; thicker material benefits from a small bevel that lets the weld penetrate rather than sit on the surface. These are unglamorous skills that no machine in this guide can compensate for, and they are why two beginners with identical welders produce work of entirely different quality within the same month.
When a Weld Fails Inspection: Deciding to Grind Out or Weld Over
Finding a bad weld in your own work is a moment of truth worth handling correctly. Surface ugliness, a lumpy start, a wandering line, can often be ground smooth and left structurally sound. Lack of fusion, cracks and porosity are different: welding over them seals the defect inside a prettier shell. The honest repair is to grind the defect out completely, back to sound metal, and reweld the section with corrected settings. It costs twenty minutes and teaches more than the original weld did.
Develop the habit of inspecting with light and, where it matters, with a simple bend or load test on practice pieces. Beginners fear inspection because it delivers bad news, but every professional’s work is inspected, and self-inspection is simply joining that culture early. The machines above will all produce welds that pass an honest home inspection when the preparation, settings and technique in this guide come together.
Workshop Safety Culture Beyond the Helmet
The helmet and gloves are the visible part of safety; the culture around them is the effective part. Keep a fire extinguisher rated for the workshop where you can reach it without passing the work, and know how to use it before you need it. Keep the welding area free of the slow accumulation of flammables that workshops attract: oily rags in a metal bin, solvents stored away from the welding zone, and a clear rule that welding stops an hour before the building is left unattended, with a final check for smouldering.
Protect other people and animals with the same seriousness: screens or warnings for anyone who might look toward the arc, pets out of the workshop entirely, and children as supervised spectators at a distance with proper eye protection or not at all. A beginner who builds this culture from the first session never has to unbuild bad habits, and the household learns that welding time is respected, equipped time rather than a hazard tolerated.
Your Second Year: Growing Into the Machine You Bought
By the second year, a beginner’s relationship with their machine changes. Settings become instinctive, the notebook fills, and projects grow in ambition. This is the moment to revisit the processes you have not used: the lift TIG or stick function of a multi-process machine, tried now with a steady hand, opens work that would have frustrated you in month one. Growth staged this way, each capability added onto a solid base, is exactly what the multi-process models in this guide are designed to support.
It is also the moment to judge the machine honestly. If it has met every project, keep it and spend the next budget on material and training. If a real, recurring limitation has emerged, power for thicker work, or a process you now use weekly that the machine does poorly, that is a justified upgrade bought from evidence. Either way, the decision will be a good one, because it rests on a year of your own welds rather than on anyone’s marketing.
Choosing Your First Real Project and Planning It on Paper
The jump from practice plate to first project deserves a plan on paper: a simple sketch with dimensions, a cutting list, the joint types marked, and the order of assembly thought through before any steel is cut. Paper is where mistakes are free. Decide where the welds will be accessible, where clamps will go, and which joint you will weld first and last, because sequence decides whether the finished piece is square or a lesson. Beginners who plan build furniture; beginners who improvise build scrap with ambition.
Choose the project by the skills it rehearses. A small table rehearses cutting, squareness and fillet welds. A storage rack adds repetition and measurement discipline. A repair rehearses preparation on imperfect metal. Any of these, finished, teaches more than an abandoned grand design, so pick the project you can complete with the machine, material and time you actually have, and let completion, not complexity, be the first year’s ambition.
Steel Buying for Beginners: Sections, Stock and Suppliers
New welders often overlook that material choice shapes the welding. Buy clean, standard sections from a supplier who will cut to length, and start with the sizes home projects actually use rather than a miscellany of offcuts in unknown alloys. Label what you bring home, because two similar-looking bars of different composition weld differently and the time to know which is which is before the arc, not during. Keep offcuts organised by type; a tidy rack is a future project’s free material and a safety improvement over a pile on the floor.
For practice, ask suppliers about offcut bins and short lengths, which provide cheap, known material for the bead drills this guide prescribes. Practising on the same material you will build with removes a variable when the real project starts. The economics are friendly: steel for a year of serious beginner practice usually costs less than the welder’s accessories did, which puts the real investment where it belongs, in your hours.
Finishing Welds: Grinding, Paint and Pride
A project is not finished when the last weld cools. Grinding is its own skill: a flap disc at the right angle smooths a weld without gouging the parent metal, and the beginner’s error is grinding a sound weld thin in pursuit of beauty. Dress only what needs dressing, keep the disc moving, and remember that a weld ground flush and a weld left as laid are both respectable finishes when each is chosen deliberately. Test any structural-looking joint before cosmetic work hides it from inspection forever.
Paint and protection complete the job and teach patience: clean, degrease, prime where the product system requires it, and let coats cure. A well-finished beginner project looks professional from across the room even where its beads were humble, and that transformation, scrap and sparks into a thing the household uses daily, is the reward that carries beginners into their second year. Finish things. The habit is worth more than any single technique in this guide.
Finding Community: Clubs, Classes and Honest Feedback
Welding learned alone plateaus where welding learned in company does not. A local class, a makerspace induction or even one experienced friend willing to watch you weld for an hour will find the faults your own eyes are trained to skip: the arc length you swear is short and is not, the travel speed your beads have been reporting all along. Seek that feedback early, while habits are wet cement, and receive it as the gift it is. Every welder you admire was corrected by somebody.
Online communities can extend that feedback if you post honestly: photographs of beads with settings and material stated invite real diagnosis, while vague questions invite folklore. Apply the same scepticism this guide teaches for gear advice to welding advice generally, and weight the words of people who show their own work, including its failures. Community, chosen well, is the cheapest accelerator a beginner can buy, and it usually costs nothing but humility.
Tack Welds: The Small Skill That Holds Everything Together
Tack welds are the unsung foundation of fabrication, and beginners underrate them because they look trivial. A good tack is small, fused and placed where it will hold alignment without fighting the final weld: at corners and midpoints, in an order that balances the pull each tack exerts as it cools. Tack everything, check for square, adjust while adjustment is still cheap, and only then commit to full welds. The frame that was tacked and measured carefully almost welds itself; the frame welded progressively from one end usually finishes as a parallelogram with excellent beads on it.
Practise tacks deliberately on scrap assemblies until placing, sizing and, when necessary, breaking and redoing them is second nature. Yes, redoing: a tack that reveals misalignment has done its job, and grinding it out to correct the fit is craftsmanship, not failure. Welders who tack patiently spend their effort once, on alignment, instead of repeatedly, on correction.
How to Talk to a Supplier, Inspector or Experienced Welder
Beginners often stay silent around expertise for fear of sounding ignorant, and lose the free education on offer. Suppliers will tell you which wire and consumables local welders actually buy, if you ask what sells rather than what is best. Experienced welders will diagnose a bead from a photograph if you bring the settings and material with it. Inspectors and instructors speak in faults with names, and every name they give you is a search term that unlocks a chapter of knowledge. Ask, record, and apply: that loop is the social machinery of the whole trade.
Bring the same honesty to those conversations that this guide asks for at the bench. Show the bad bead, not just the good one. State what you changed and what happened. People help welders who report accurately, because accurate reports can actually be answered. The beginner who learns to ask well in the first year will never lack for teachers in the tenth.
Frequently Asked Questions
Is it right for beginners?
Check the features and manual.
Do I need extras?
Often protective gear or accessories.
How do I store it?
Dry and covered.
Should a beginner pick gas or gasless welding?
Gas gives cleaner welds and less spatter, and is best in a sheltered workshop. Flux-core avoids a gas bottle and tolerates wind and dirtier metal, but needs more cleanup. Many beginners choose a machine that can do both.
Can I run a MIG welder on a normal household outlet?
Some machines are designed for 120-volt outlets, with limits on thickness. Others need 240 volts. Check the listing's input requirements and your circuit rating.
What does duty cycle mean?
It is the share of a ten-minute period a machine can weld at a given current before cooling. Lower duty cycles mean more pauses. It matters most for long welds on thick material.
Why is my weld full of holes?
Porosity usually comes from poor shielding gas coverage, wind, dirty metal or damp wire. Clean the work, check the gas flow and shelter the weld area.
Do I need a special helmet?
Yes. Use a welding helmet with the correct shade and good eye protection. Auto-darkening helmets are popular with beginners. Never look at the arc without protection.
How often should I replace the contact tip?
When it is worn, clogged or the wire feeds erratically. The interval depends on use and settings. Keep spares on hand.
Can I weld aluminum with a beginner MIG welder?
It needs different wire, gas and often a spool gun, and not every machine supports it. Check the listing and manual before attempting it.
Bottom Line
Dual-voltage 3-in-1 machines suit most beginners.
More Workshop Guides
- Best 140A Flux Core Welders for Home Shops
- Best Waterproof Generator Covers
- Flux Core or MIG Welder? A Beginner Guide